Use an Acceptance Individuals Chart to detect when the out-of-specification percentage might exceed an acceptable level. Use when you have continuous data that are individual observations not in subgroups.
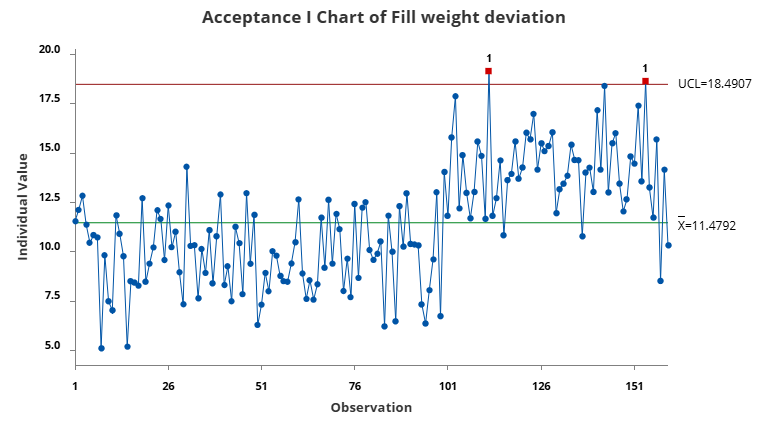
Two observations are above the upper acceptance control limit. These points indicate that the process shifted far enough toward the upper specification limit that more than 1% of the process output might exceed the specification limit.
Note
The process variation must be in control before you assess the process center using an Acceptance Individuals chart because the acceptance control limits are calculated using an estimate of process variation. If the process variation is not in control, the acceptance control limits are not reliable and Minitab might produce a false out-of-control signal. Use a moving range chart to determine whether the process variation is in control.
Where to find this control chart
To create an Acceptance Individuals chart, choose .
When to use an alternate control chart
- If you can collect data in subgroups, use Acceptance Xbar Chart.
