In This Topic
Plotted points
Each plotted point,  , represents the mean of the observations for subgroup,
 .

Notation
| Term | Description |
|---|---|
| xij | jth observation in the ith subgroup |
| ni | number of observations in subgroup i |
Center line
The center line represents the process mean ( ). If you specify a historical value for an analysis that allows a
historical value, then the analysis uses the historical value. Otherwise, the
analysis uses the average from your data,
 , which is calculated as follows:

Notation
| Term | Description |
|---|---|
 | sum of all individual observations |
 | total number of observations |
Control limits
Lower control limit (LCL)
The value of the lower control limit for each subgroup, i, is calculated as follows:

Upper control limit (UCL)
The value of the upper control limit for each subgroup, i, is calculated as follows:

Notation
| Term | Description |
|---|---|
| μ | process mean |
| k | parameter for Test 1 (The default value is 3 for analyses that allow custom values. The value is 3 for analyses that do not allow custom values.) |
| σ | process standard deviation |
| ni | number of observations in subgroup i |
Extended control limits: Between/within approach
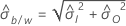
Use the between/within approach to calculate extended control limits from within-subgroup and between-subgroup standard variation.
Subgroup size > 1

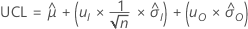
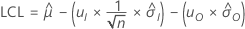
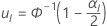
Where uI and uO are quantiles of the standardized normal distribution.
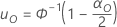
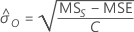
Notation for between/within approach
| Term | Description |
|---|---|
| μ̂ | estimate of process mean |
| σ̂I | estimate of within-subgroup standard deviation |
| σ̂O | estimate of between-subgroup standard deviation. If there is only 1 subgroup, then σ̂O = 0. |
| n | subgroup size when the subgroup size is greater than 1 |
| αI | false alarm probability for within-subgroup standard deviation |
| Φ-1 | the inverse cumulative distribution function of the standard normal distribution |
| αO | false alarm probability for between-subgroup standard deviation |
| MSS | the mean square associated with subgroup-to-subgroup variation |
| MSE | mean squared error. The within-subgroup mean square subtracted from the subgroup mean square before estimating the between-subgroup standard deviation component. |
| C | coefficient for the expected mean square for subgroups as a random
factor. For the calculations of expected mean squares and for information on unbalanced or more complex models, see Montgomery1 and Neter2.
|
Extended control limits: Min/max mean approach
Use the min/max mean approach to calculate extended control limits from the minimum and maximum group means.
Subgroup size > 1

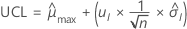
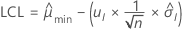
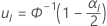
Where uI is the quantile of the standardized normal distribution.
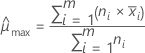
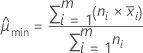
Notation for min/max approach
| Term | Description |
|---|---|
| μ̂ | estimate of process mean |
| μ̂max | estimate of the maximum process mean. Using the subgroup size, this estimate is the weighted average of the m largest subgroup means. If the analysis specifies to use more subgroups than are in the data, m is the number of subgroups. |
| μ̂min | estimate of the minimum process mean. Using the subgroup size, this estimate is the weighted average of the m smallest subgroup means. If the analysis specifies to use more subgroups than are in the data, m is the number of subgroups. |
| m | number of subgroup means to average |
| σ̂I | estimate of within-subgroup standard deviation |
| n | subgroup size when the subgroup size is greater than 1 |
| Φ-1 | the inverse cumulative distribution function of the standard normal distribution |
| αI | false alarm probability for within-subgroup standard deviation |
Standard deviation for extended limits
When extended limits are selected, use the following standard deviation for stored variation values and additional sigma limits.